
- 100+ production machines — 3-axis (50+), 4-axis (20+), 5-axis (20+), 25+ lathes, 7+ grinders, plus 20+ inspection instruments.
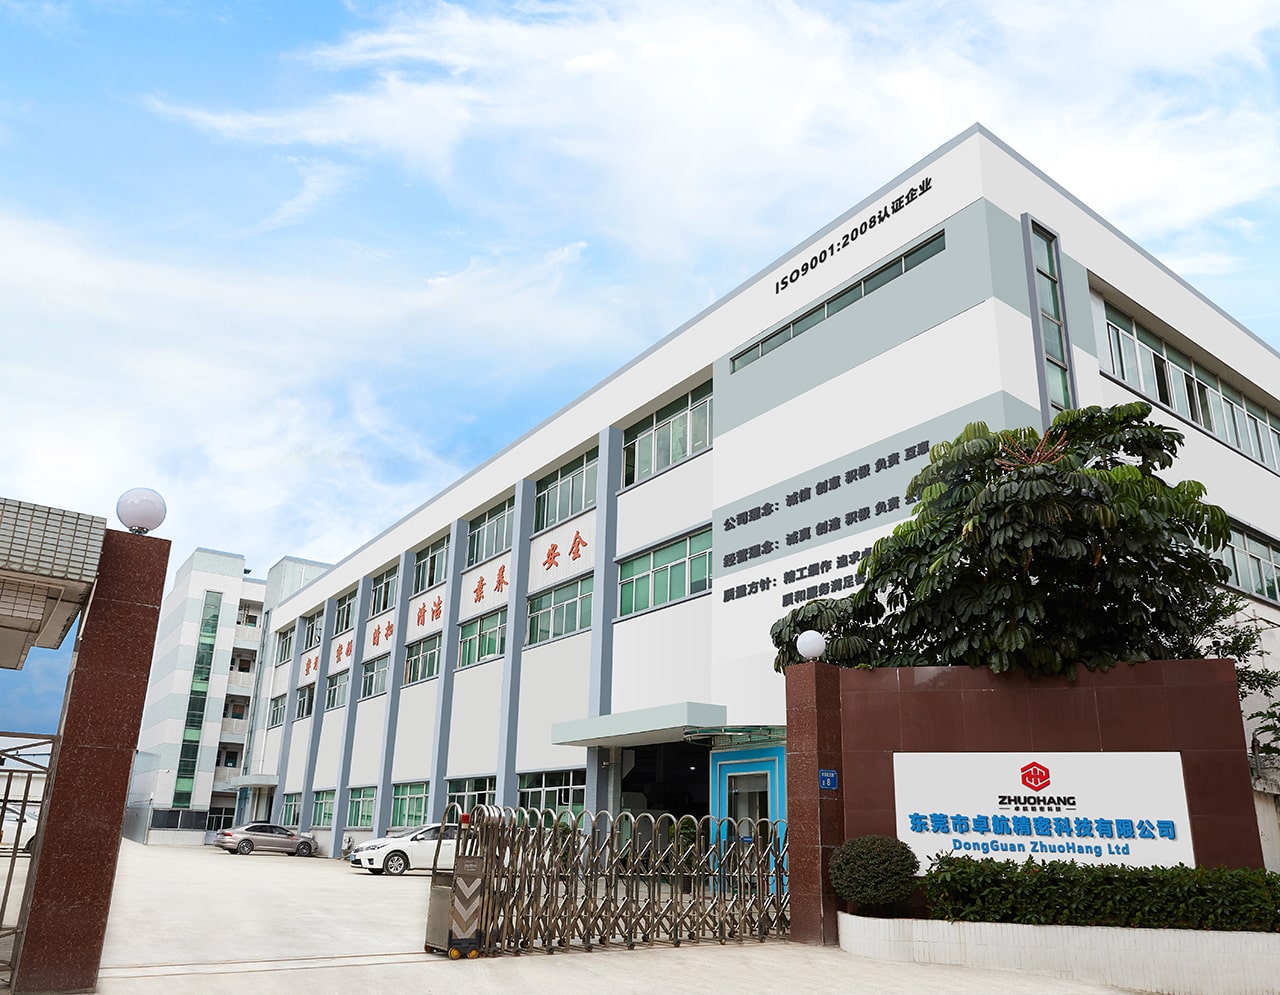
- 6,800 m² facility in Hengli Town, Dongguan, founded 2005, run by 100+ staff.
- 80%+ skilled technicians, 60% with 5–10 years on the floor, founder with 28 years in machining.
- ISO 9001, IATF 16949, ISO 14001 — documented, third-party-surveilled systems.
Why does the factory behind the quote matter to your cost?
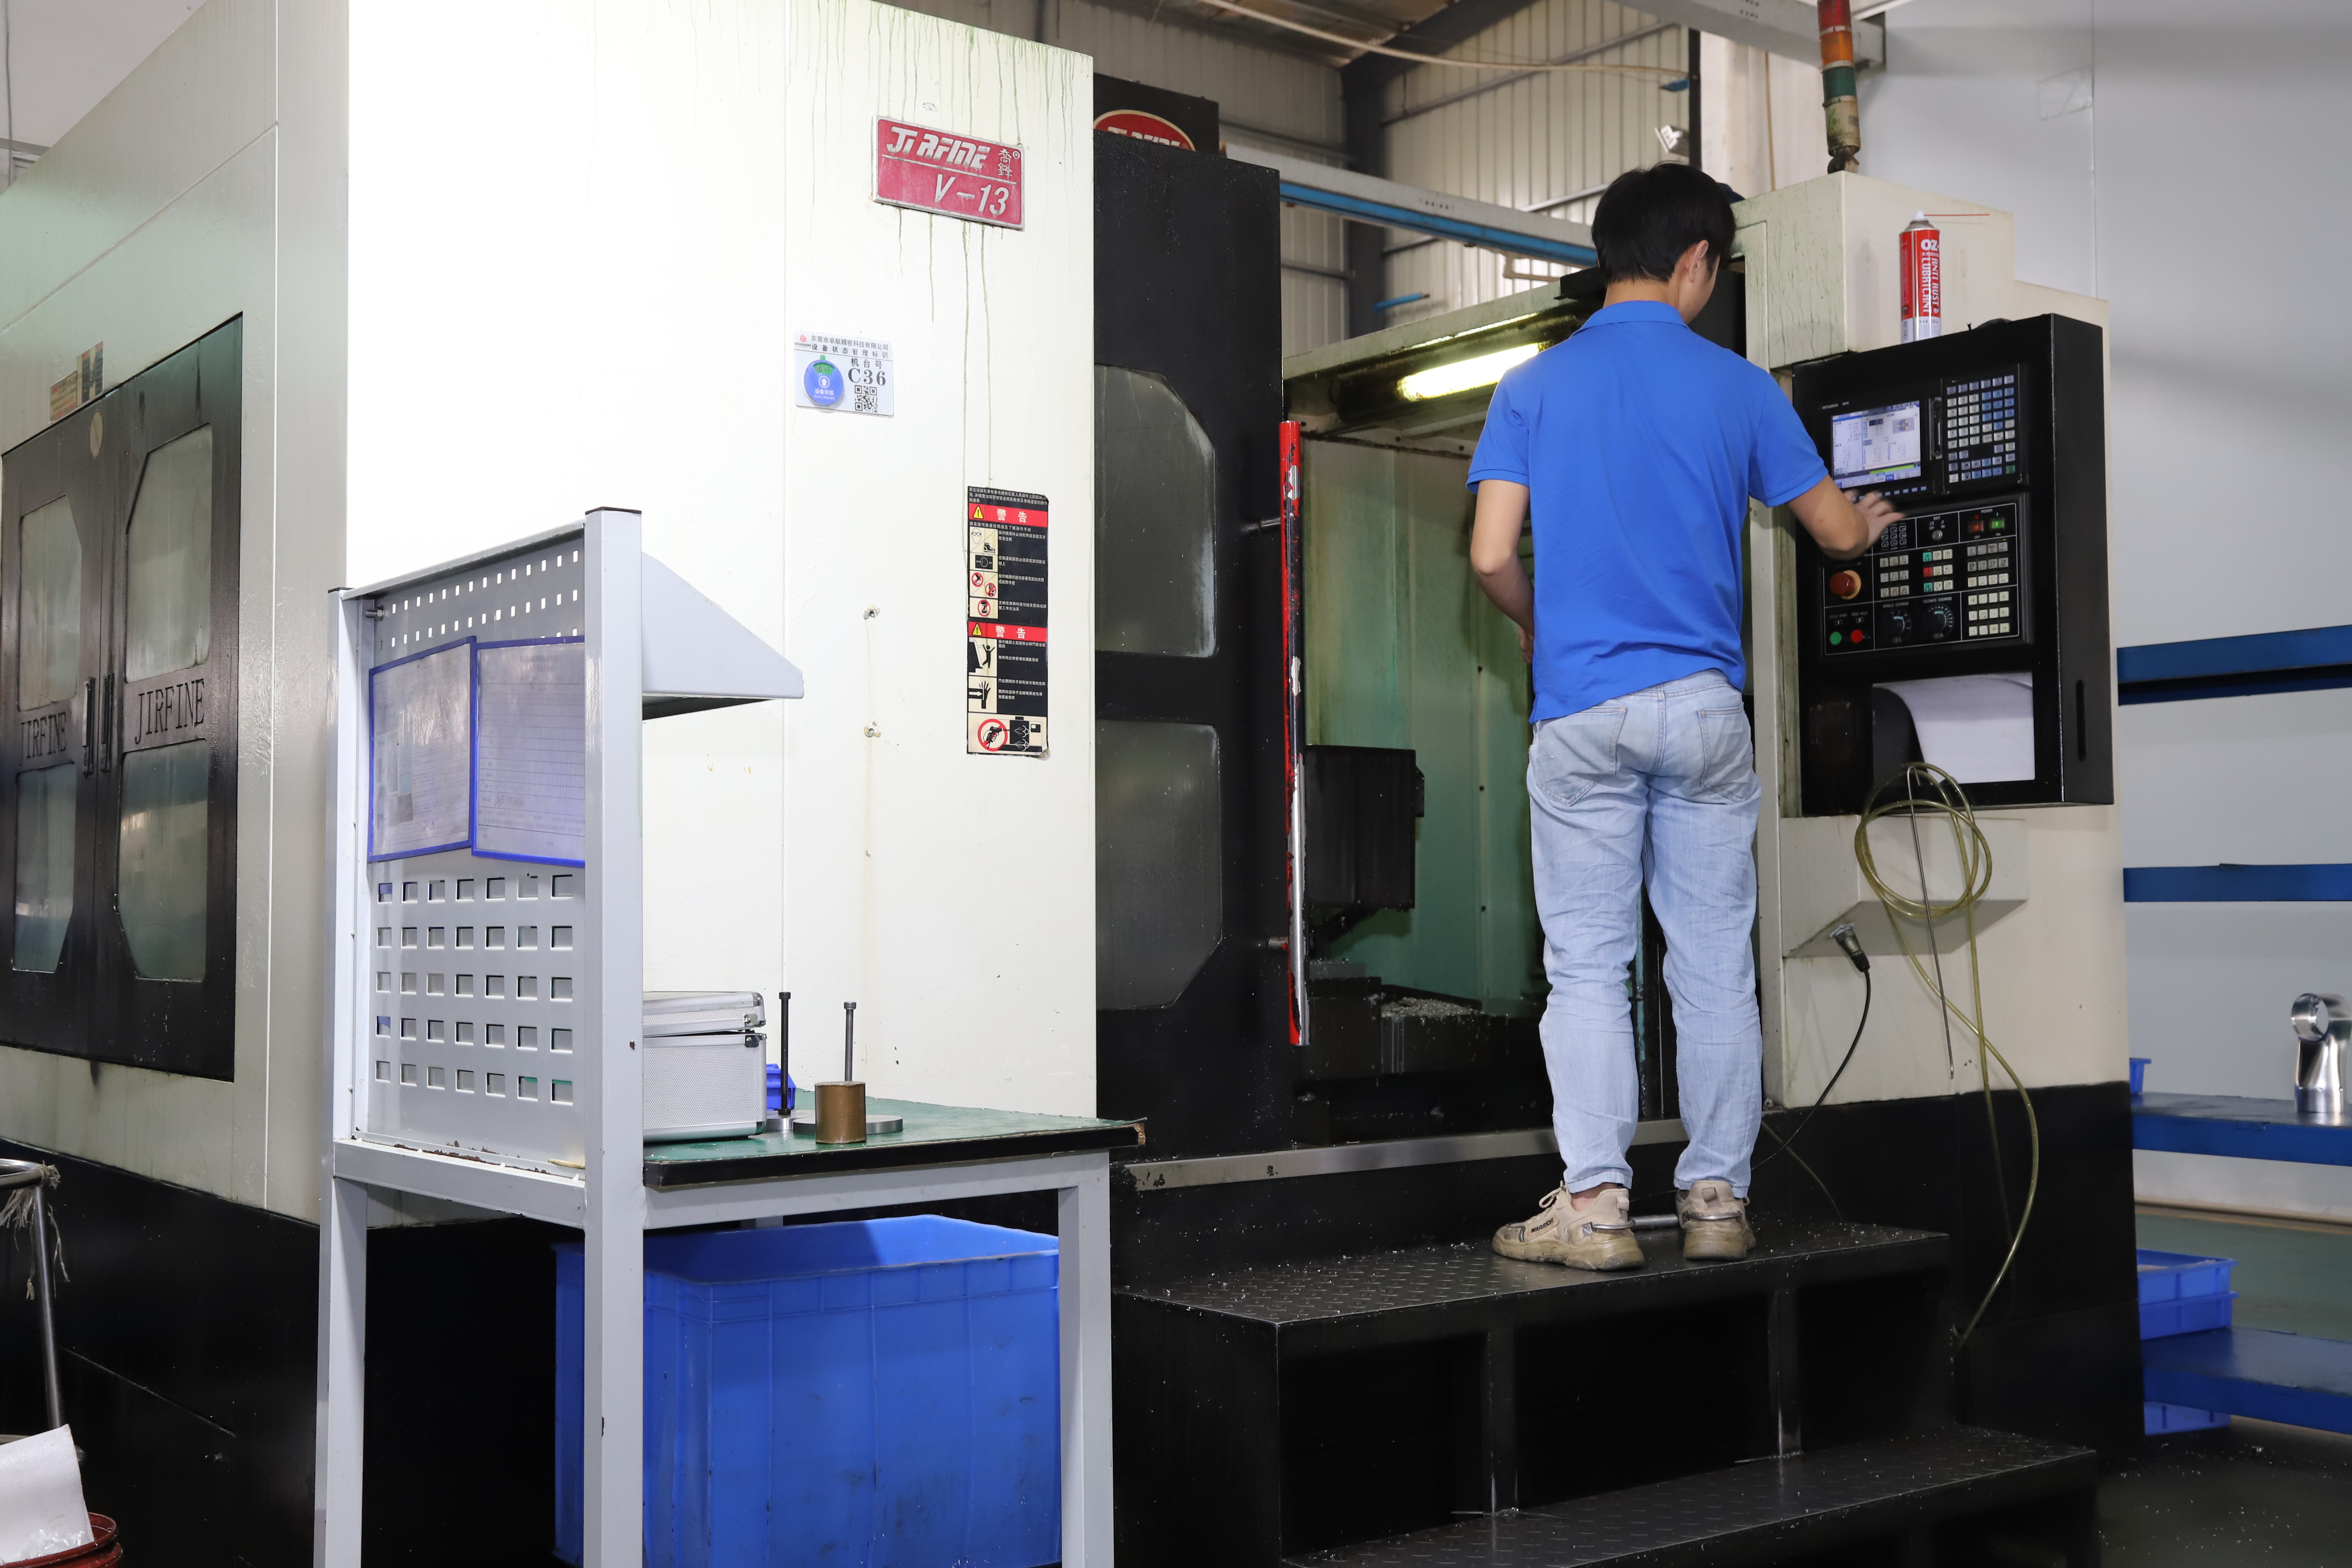
When you buy machined parts, you are not really buying the parts — you are buying the factory that makes them, because that is where your cost is decided. The factory sets your lead time, holds your tolerance, and controls the scrap and rework that either stays on its floor or lands on your invoice. A reseller with no floor of its own can quote you a price, but it cannot control the schedule or the quality behind that price, and that gap between quote and reality is exactly where your hidden cost lives.
That is why the sensible first question in sourcing is not "what does it cost" but "who actually makes it." A real factory answers with a machine list, a floor you can walk, and a quality system you can audit. Everything after that — price, lead time, tolerance — follows from the factory's capability, so evaluating the factory is evaluating the cost before the invoice is ever written.
What does a floor of 100-plus machines mean for your lead time and cost?
Machine count is not vanity; it is the difference between a shop that can absorb your order and one that queues it behind someone else's. A floor of 100+ production machines has the slack to start your job when you need it rather than when a machine frees up, which keeps your lead time predictable and your schedule intact. It also means redundancy: if one machine goes down, another takes the job, and your date does not move with it.
The mix matters as much as the total. 50+ 3-axis, 20+ 4-axis, and 20+ 5-axis centers cover prismatic parts; 25+ lathes cover round parts up to Ø720 × 1280 mm; mill-turn centers handle single-setup complex geometry; and 7+ grinders hold ±0.002 mm finishes. That breadth means your part stays on one floor for most operations, which shortens the chain and removes the mark-up and risk of subcontracted steps.
How does facility size and scale protect your schedule?
Scale is schedule insurance. A 6,800 m² facility running 100+ staff and turning out over a million parts a year has seen the volume, the variety, and the problems that a smaller shop has not. That experience shows up in the details a buyer rarely thinks about until they go wrong: how to sequence a complex part with 10–20 process steps, how to schedule surface finishing without stalling the batch, how to absorb a rush order without breaking the queue.
For you, scale means the factory is still standing, still staffed, and still shipping when your order matters most. A supplier that disappears mid-program costs you a switch; a factory with two decades of continuity — founded in 2005 — is the opposite of that risk. Scale is not a number on a wall; it is the probability that your order ships on time, every time, for the life of the program.
Who actually runs the machines?

The people on the floor are the factory, and their stability is your quality stability. Here more than 80% of the workforce are skilled technicians, 60% have been with the factory for five to ten years, and the founder brings 28 years in machining. That continuity means the person running your part has run ten thousand parts like it before, and the setup knowledge lives in the room rather than walking out the door.
Turnover is a hidden cost you inherit: a rotating cast of operators re-learns your drawing on your time and your scrap. A stable, experienced floor does the opposite — it builds the tolerance and the speed into muscle memory, so your repeat orders come back identical to the first. When you evaluate a factory, ask how long its machinists stay. The answer predicts more about your parts' consistency than any brochure.
What equipment verifies the parts?
A factory that machines to a micron but measures with a ruler cannot vouch for its own tolerance. The inspection bench here is the same class of equipment a buyer would use to audit the place: Hexagon GLOBAL S CMMs for dimensional verification, vision measuring machines, a gear measuring center, a KEYENCE VK-X3000 laser microscope, a SURFCOM 1800D for profile and roughness, and an XRF spectrometer for material composition. In total, 20+ inspection instruments sit alongside the machines, not in a separate room two weeks away.
The point of that bench is not to look impressive — it is to produce the reports that let you trust the parts without opening every box yourself. A CMM report with measured values against your drawing, an SPC chart with a computed Cpk, a material certificate matched to an XRF check: those are the documents that turn a promise into a fact, and they are produced on the floor, not promised on the phone.
Which certifications does the factory hold?
Certification is a pre-audit you get for free: it tells you the factory already runs a documented system under third-party surveillance, so you do not have to build that confidence from scratch. This factory holds three, with scope stated honestly.
| Standard | Certificate number | Scope |
|---|---|---|
| ISO 9001:2015 | 116024/A/0001/UK/En | Machining of metal parts |
| IATF 16949:2016 | 131941/A/0001/SM/En | Manufacture of CNC metal machining parts (excludes product design, Clause 8.3) |
| ISO 14001:2015 | 116024/B/0001/UK/En | Environmental management related to machining of metal parts |
Honest scope note: IATF 16949 excludes product design under Clause 8.3. We are a build-to-print manufacturer — if your program needs us to own design responsibility, say so up front and we will scope it accordingly rather than over-promise.
Where is the factory and why does location matter?
The factory sits at No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470 — in the Pearl River Delta, the densest manufacturing region in the world. Location is a quiet cost input: it shortens the supply of raw stock, keeps secondary processes like anodizing and heat treatment within reach, and puts the factory minutes from the freight lanes that move parts to the ports.
For an overseas buyer, that geography shows up as shorter, more predictable lead times and fewer delays between the machine and the ship. A factory in a supply-chain-rich region is a factory that can get material and finishing without waiting weeks, and that speed is ultimately a line on your cost of ownership — a part that ships sooner is a part that never forces an expedite.
How does the factory trace every part?
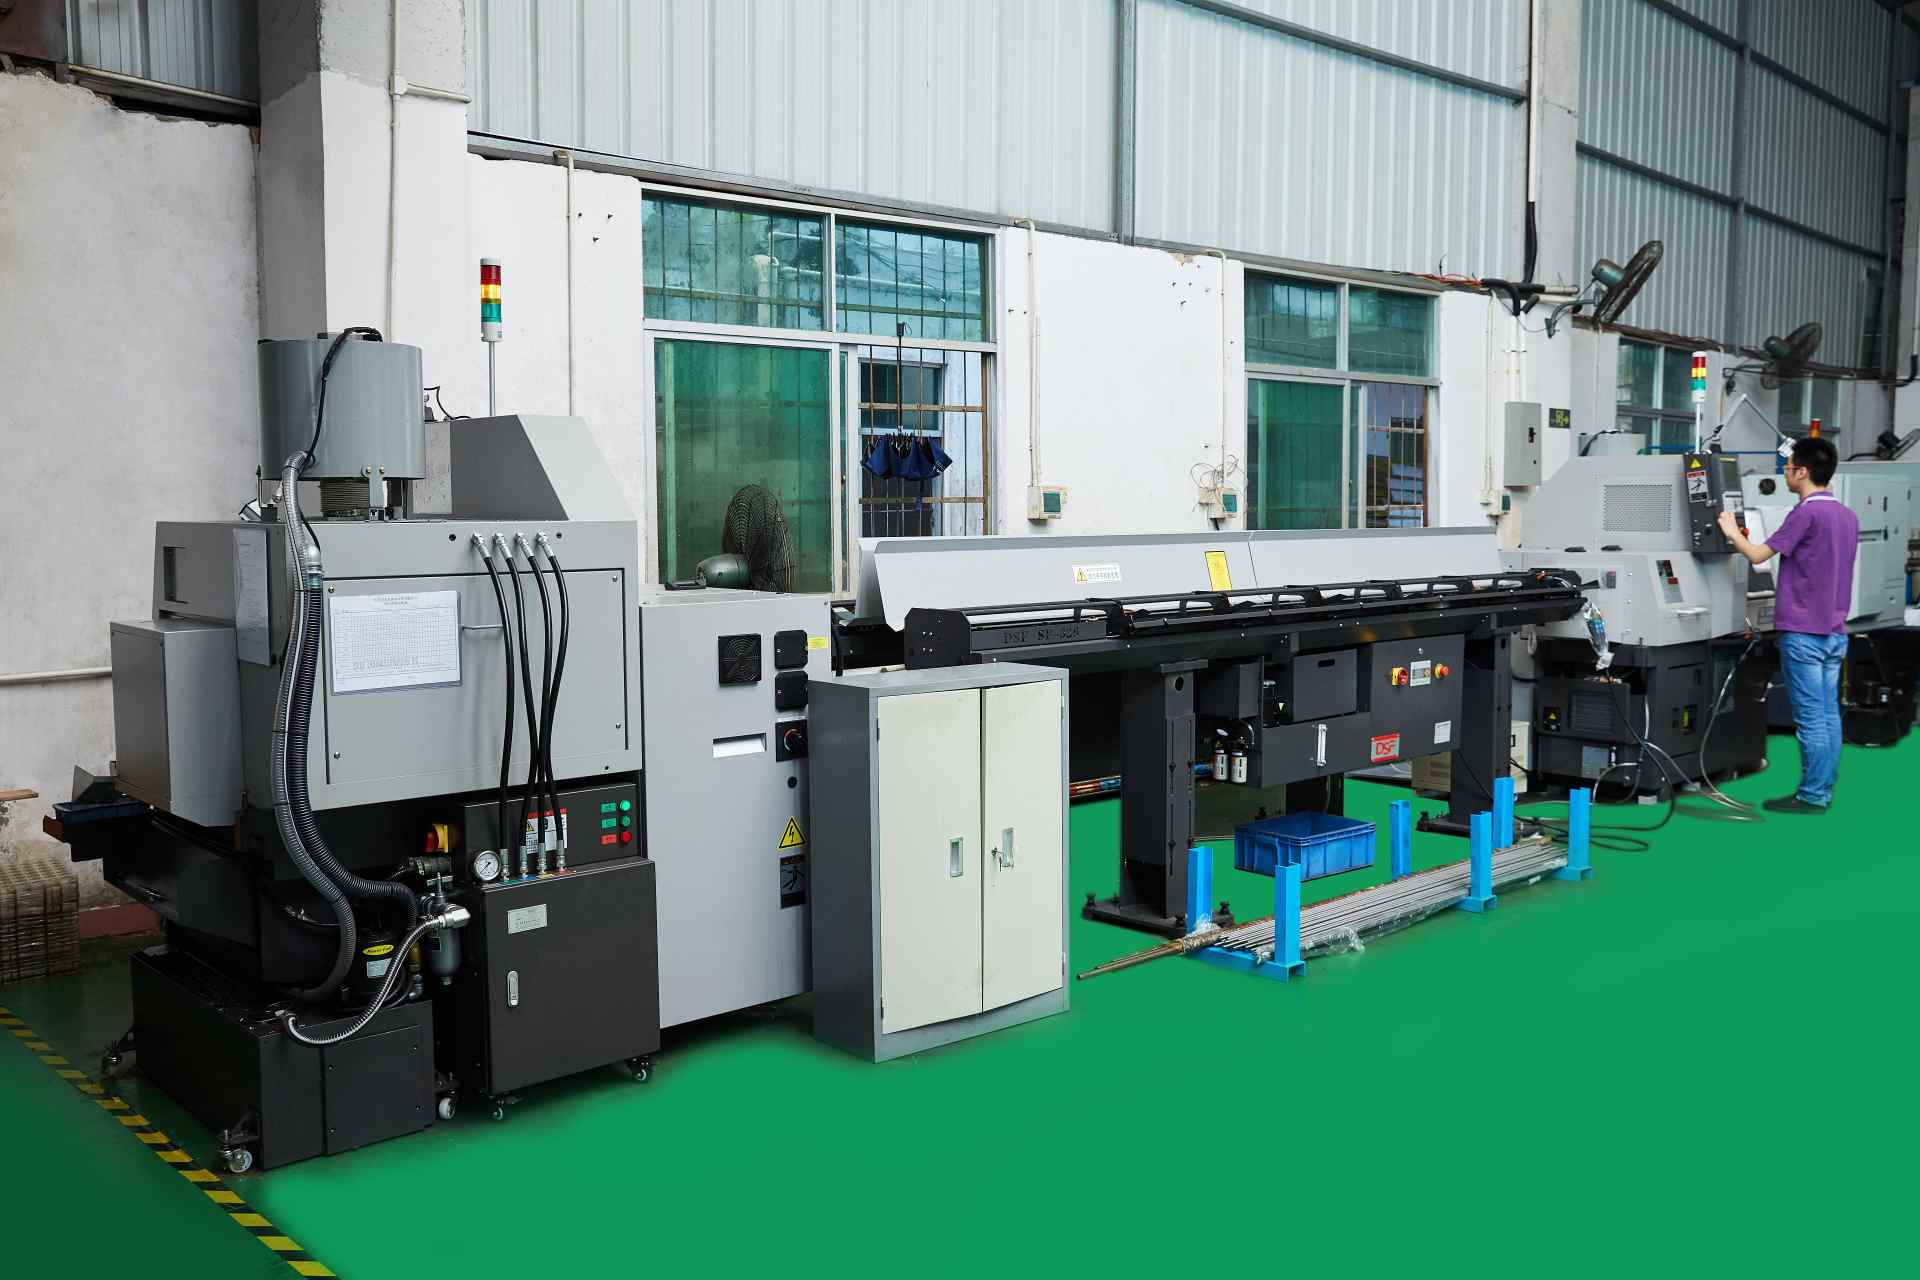
Traceability is what separates a factory that can contain a problem from one that has to guess. The MES/ERP system records the full chain on every lot — raw material source and usage, process parameters, machine data, production batch, machining time, operator, and inspection results. When a non-conformance surfaces, the factory can point to the exact lot, machine, and operator, and isolate the affected parts rather than replacing an entire order.
For regulated buyers that traceability is a requirement; for everyone else it is cheap insurance against the costliest kind of failure — the one where you cannot prove which parts are bad and have to treat them all as suspect. The chain begins with an XRF check of incoming material against its mill certificate, and it runs on every job, not just the ones that demand it.
What should you verify about any factory before ordering?
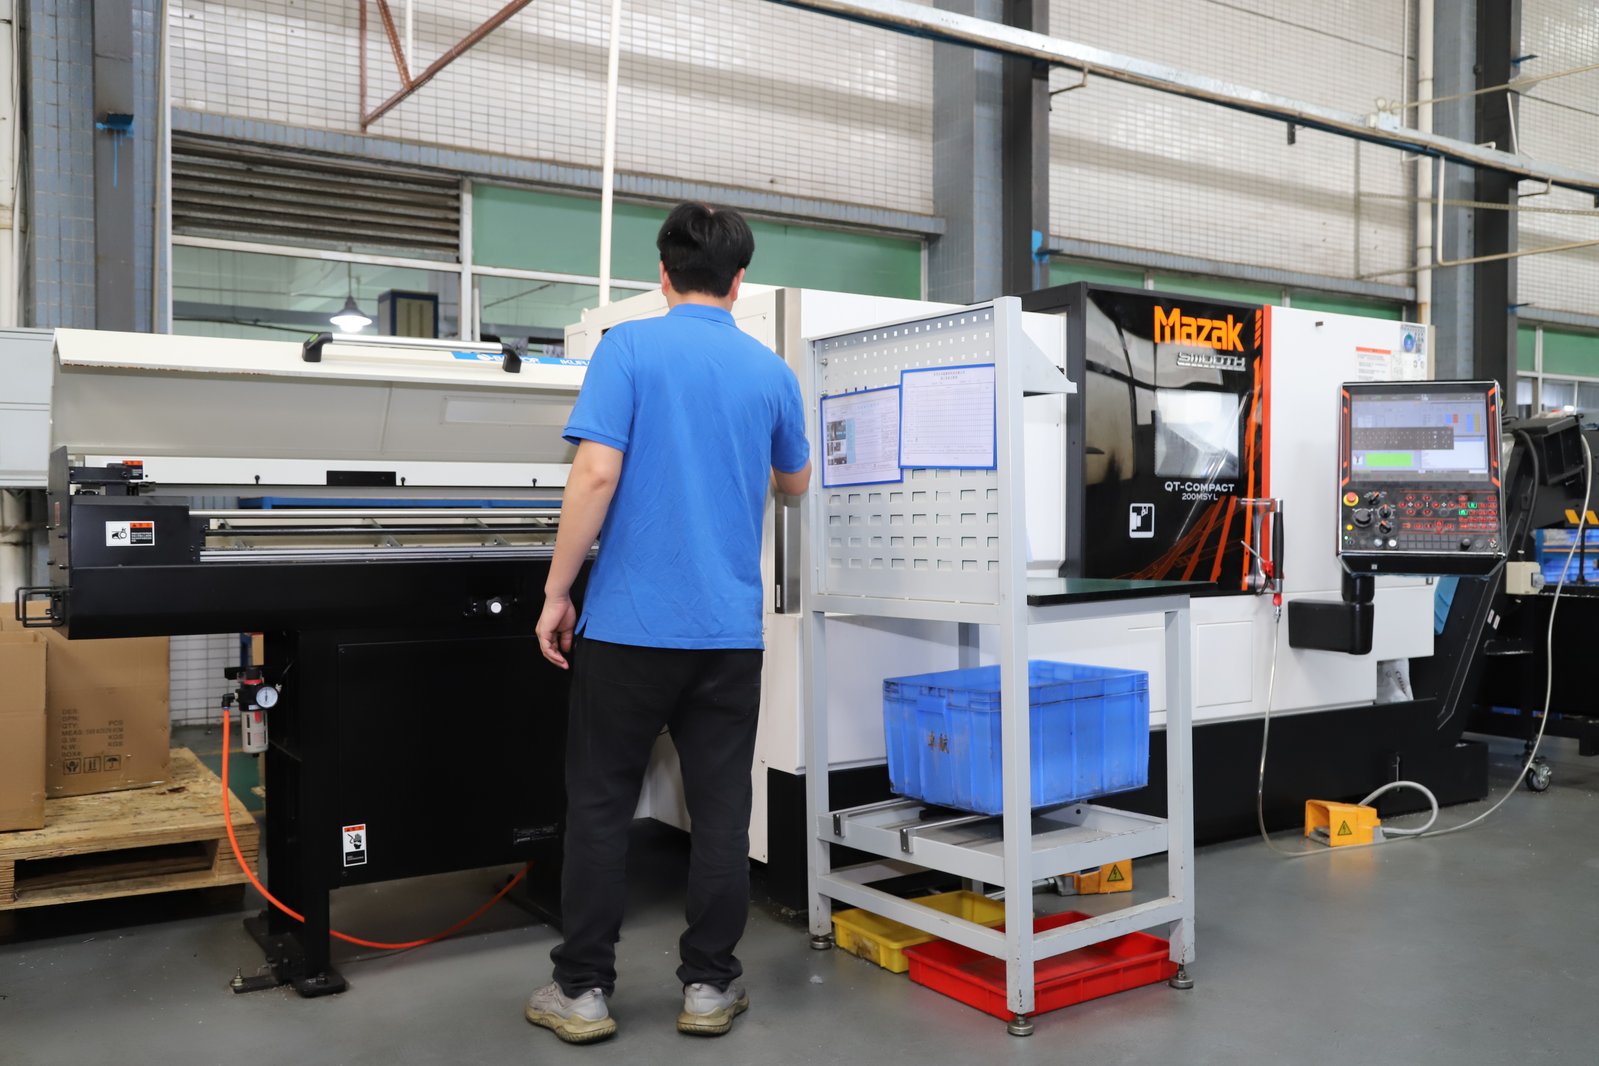
Whether you buy from this factory or another, the checks below separate a real manufacturer from a trading desk, and they cost you nothing to run. Apply them to any supplier — including this one — before you commit.
- Ask for a live video walk-through of the running floor. A real factory says yes in minutes; a reseller deflects to samples and slides.
- Ask for the machine list with brands and axis counts. Then count the machines yourself on the walk-through.
- Ask for a CMM or SPC report from a real job. A capability statement is a claim; a measured report is a fact.
- Ask for the certificate numbers. Real ISO/IATF certificates can be checked with the registrar.
- Ask how long the machinists stay. Turnover is a hidden cost you inherit in scrap and rework.
Run those five checks and the factory behind the quote stops being a mystery, which is the whole point, because a factory you cannot see is a cost you cannot control. Visits and audits are welcome here, and the answer to every check is available in writing before you spend a dollar.
How do the machine brands affect your total cost?
The brand on a machine is not decoration; it is a predictor of the machine's repeatability, its uptime, and how well the shop can hold a tolerance over a long run. A floor built on Mazak, Brother, TSUGAMI, and Sodick machines — with Citizen and Star turning centers where the work calls for it — carries a different cost profile than a floor of mixed, older, or off-brand equipment, because a machine's thermal stability and control quality decide how often a part falls out of spec in the middle of a batch.
From your seat, machine quality shows up as a lower hidden cost. A rigid, thermally stable machine holds size for longer between offsets, which means fewer in-process corrections, less scrap, and a steadier Cpk. That steadiness is what keeps your defect count low without your having to inspect every part yourself. When you audit a factory, the machine list — brand, model, and axis count — is the closest thing to reading the floor's cost structure in advance.
| Equipment class | Representative brands | What it means for your parts |
|---|---|---|
| 3-axis / 4-axis / 5-axis milling | Mazak, Brother | Prismatic parts from simple brackets to 5-axis contours in one setup |
| CNC turning | TSUGAMI, Citizen, Star | Round parts to Ø720 × 1280 mm with stable size over long runs |
| EDM (sinker / wire) | Sodick | Sharp corners, fine details, and hardened materials a cutter cannot reach |
How does production scheduling protect your delivery date?
A delivery date is a promise the production schedule has to keep, and the schedule is what separates a date you can plan around from a date that slips. A factory with enough machine capacity and a disciplined planning system can slot your job into a real queue, sequence the operations, and tell you a date it can actually hold. A factory without that discipline quotes a date and hopes.
The schedule also decides how a rush order is absorbed. When a machine goes down or a priority job lands, a floor with slack can re-route the work without moving your date; a floor running at the edge of its capacity pushes everything back. That slack — the difference between a hundred-odd machines fully booked and a hundred-odd machines with room to breathe — is invisible on a quote and decisive on a deadline. It is part of what you are paying for when a supplier's lead time holds.
What this shop actually runs
Ask for capability evidence and the answer should be specific. The facility behind this guide runs 100+ CNC machines on a 6,800 m2 floor in Dongguan, China, with 100+ staff. The machine list, by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Best for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Best for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Best for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Best for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Best for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerances held: milling ±0.003 mm, turning ±0.002 mm, grinding and wire EDM ±0.002 mm. Capability: Ppk >= 1.67 initial and Cpk >= 1.33 in production on key characteristics.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, clause 8.3 design excluded, disclosed openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, USCC 91441900MA4UWT6X39, established 2005.
Service area: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — built in China, shipped worldwide.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Want to see the factory before you commit?
Email [email protected] or call +86 13126536955 to arrange a visit or a live video walk-through.
Frequently Asked Questions
Why does the factory behind the quote matter to my cost?
In short, The factory is where your lead time, quality, and rework are decided. A reseller with no floor of its own cannot control schedule or tolerance, and that risk lands on your cost.
How big is the factory and how many machines does it run?
The facility covers 6,800 m² in Hengli Town, Dongguan, and runs 100+ production machines — 50+ 3-axis, 20+ 4-axis, 20+ 5-axis, 25+ lathes, and 7+ grinders — plus 20+ inspection instruments. Founded in 2005, it employs 100+ people.
Who actually runs the machines?
In short, More than 80% of the workforce are skilled technicians, 60% have been with the factory for five to ten years, and the founder brings 28 years of industry experience. That continuity means your parts are machined by people who know the process, not by a rotating cast.
Where is the factory located?
No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470. Dongguan sits in the Pearl River Delta manufacturing region, which shortens material supply and freight logistics compared with more remote sites.
Which certifications does the factory hold?
In short, ISO 9001:2015 (No. 116024/A/0001/UK/En), IATF 16949:2016 (No.
How does the factory trace every part?
In short, An MES/ERP system records raw material source and usage, process parameters, machine data, production batch, machining time, operator, and inspection results for every lot. If a non-conformance surfaces, the factory can identify the exact lot, machine, and operator.
What should I verify about any factory before ordering?
In short, Ask for a live video walk-through of the running floor, the machine list with brands and axis counts, a real CMM or SPC report from a past job, and certificate numbers you can check with the registrar. A factory that welcomes those checks is one you can scale with.
Can I visit the factory?
Yes. Factory visits and audits are welcome, and the address is No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470. Contact [email protected] to arrange a visit or a live video walk-through.
Standards referenced on this page
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- ISO 14001 — Environmental management systems — Requirements with guidance for use
- ASTM E8/E8M-21 — Standard Test Methods for Tension Testing of Metallic Materials